Lathe SFM to RPM Formula: Surface Speed Calculation Guide
Convert lathe SFM to spindle RPM using workpiece diameter. Includes cutting speed formulas, material charts, and feed rate calculation tips.
When standing in front of a CNC lathe or manual milling machine, converting surface feet per minute into exact spindle RPM is urgent. Dialing in the wrong spindle speed burns expensive carbide tooling or ruins critical workpiece tolerances. The formula to calculate lathe spindle RPM from SFM is RPM = (SFM × 3.82) / Diameter. Here is the complete machining speed guide and cutting calculation breakdown.
In manufacturing and metalworking, cutting tools perform best within a narrow range of linear peripheral velocity called Surface Feet per Minute (SFM). Because machine spindles accept input commands in revolutions per minute (RPM), machinists must translate SFM into rotational velocity based on the workpiece or cutter diameter.
You can calculate custom cutting parameters using the interactive tool below, or explore our reference library of standard rotational velocities in the conversions directory:
The Core Lathe SFM to RPM Formula
Tooling manufacturers specify recommended cutting speeds in surface feet per minute according to material hardness and tool coating. Guidelines established by the American Society of Mechanical Engineers (ASME) and machining standards from the International Organization for Standardization (ISO) define linear surface velocity as:
SFM = (π × Diameter in inches × RPM) / 12To calculate required lathe spindle speed, rearrange the equation to solve for RPM:
RPM = (SFM × 12) / (π × Diameter)Because 12 / π ≈ 3.8197186, machinists use the universal rule-of-thumb constant 3.82:
RPM = (SFM × 3.82) / DiameterWhere:
- RPM is spindle rotational velocity in revolutions per minute.
- SFM is the manufacturer recommended surface speed in surface feet per minute.
- Diameter is the outer diameter of the workpiece (on a lathe) or the cutter (on a mill) in inches.
- 3.82 is the simplified conversion factor
12 / π.
For example, turning a 2.0-inch diameter 4140 steel bar with a carbide insert rated at 400 SFM requires:
RPM = (400 × 3.82) / 2.0 = 1528 / 2.0 = 764 RPMFor metric machining calculations where cutting speed is specified in meters per minute (m/min), review our comprehensive guide on rpm to linear velocity.
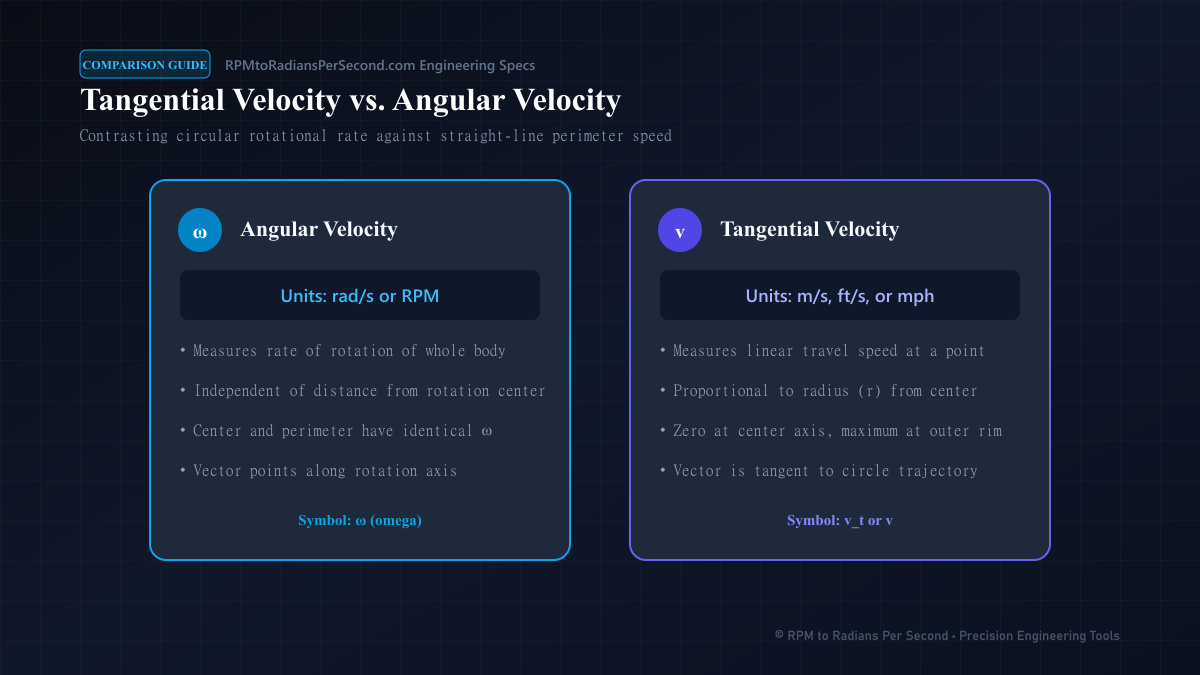
Machining Cutting Speed Chart by Material
The table below outlines recommended baseline SFM and calculated spindle RPM across standard stock diameters for common manufacturing metals using coated carbide tooling:
| Workpiece Material | Recommended SFM | 0.50" Dia (RPM) | 1.00" Dia (RPM) | 2.00" Dia (RPM) | 4.00" Dia (RPM) |
|---|---|---|---|---|---|
| 6061-T6 Aluminum | 1,000 SFM | 7,640 RPM | 3,820 RPM | 1,910 RPM | 955 RPM |
| Mild Carbon Steel (1018) | 450 SFM | 3,438 RPM | 1,719 RPM | 860 RPM | 430 RPM |
| Alloy Steel (4140 Annealed) | 350 SFM | 2,674 RPM | 1,337 RPM | 669 RPM | 334 RPM |
| 304 Stainless Steel | 250 SFM | 1,910 RPM | 955 RPM | 478 RPM | 239 RPM |
| Titanium (Ti-6Al-4V) | 150 SFM | 1,146 RPM | 573 RPM | 287 RPM | 143 RPM |
| Inconel 718 | 80 SFM | 611 RPM | 306 RPM | 153 RPM | 76 RPM |
Notice that as part diameter doubles, required spindle RPM halves to maintain constant surface speed. For background on how electric spindle motors deliver power across varying RPM ranges, consult our guide on standard motor RPMs.
Metric Conversion: Cutting Speed (m/min) to RPM
International manufacturing standards documented by the NIST Guide to SI Units specify cutting velocity in meters per minute ( in m/min) and part diameter in millimeters ( in mm).
The metric cutting speed formula is:
RPM = (V_c × 1000) / (π × D)Because 1000 / π ≈ 318.31, the simplified metric formula is:
RPM = (V_c × 318.3) / DWhere:
- V_c is cutting speed in meters per minute (m/min).
- D is workpiece or tool diameter in millimeters (mm).
- 318.3 is the dimensional constant converting millimeters to meters while dividing by π.
To convert calculated spindle speeds directly into radians per second for physics simulation or vibration analysis, explore our foundation article on rpm to radians per second.
Spindle Power and Torque Requirements in Turning
Operating at calculated RPM must remain within the torque and horsepower capabilities of the machine spindle motor. Cutting force generates tangential resistance at the tool tip:
Power (HP) = (Tangential Cutting Force in lbs × SFM) / 33,000At low RPM on large diameter workpieces, lathe spindles must produce massive shaft torque to prevent stalling. To model spindle gearbox step-downs and motor torque curves, read our references on gear ratio rpm calculator and rpm and torque to horsepower.
Python Tooling Calculator Script
Automated CNC post-processors and tool management software compute spindle RPM and feed rates automatically. University engineering courses, including manufacturing labs published on MIT OpenCourseWare, teach students to automate these speed calculations:
import math

def calculate_lathe_rpm(sfm: float, diameter_inches: float) -> float:
    if diameter_inches <= 0:
        raise ValueError("Workpiece diameter must be greater than zero.")
    return (sfm * 12.0) / (math.pi * diameter_inches)

cutting_speed = 350.0  # SFM for 4140 steel
workpiece_dia = 1.75   # 1.75 inch diameter

spindle_speed = calculate_lathe_rpm(cutting_speed, workpiece_dia)
print(f"Spindle Speed: {spindle_speed:.1f} RPM") # Output: 764.0 RPM
Calculating Feed Rate (IPM) from Spindle RPM
Once you calculate spindle RPM from SFM, the next critical machining step is determining the linear feed rate. Tool manufacturers specify chip load as feed per revolution (IPR) for lathe turning or feed per tooth (FPT) for milling cutters.
For lathe turning operations:
Feed Rate (IPM) = Spindle RPM × Feed per Revolution (IPR)For milling operations with rotating multi-flute end mills:
Feed Rate (IPM) = Spindle RPM × Flutes × Feed per Tooth (FPT)For example, when turning a steel shaft at 764 RPM with a recommended finishing chip load of 0.008 inches per revolution:
Feed Rate = 764 RPM × 0.008 IPR = 6.11 inches per minute (IPM)Pairing correct spindle RPM with proper chip load prevents work hardening in stainless steels, prevents premature tool flank wear, and maintains excellent surface finish. When cutting aggressive alloys like titanium or nickel superalloys, maintaining consistent chip thickness prevents cutting edge rubbing and localized heat buildup. Always verify manufacturer chip load recommendations before engaging automatic power feed on CNC equipment.
To explore broader kinematics and rotational velocity transformations, read our complete angular velocity guide.
Frequently Asked Questions
What is the formula to convert lathe SFM to RPM?
The formula is RPM = (SFM × 3.82) / Diameter, where SFM is surface feet per minute and Diameter is workpiece diameter in inches. The constant 3.82 equals 12 / π.
What does SFM stand for in machining?
SFM stands for Surface Feet per Minute. It measures the linear distance in feet that a point on the perimeter of the rotating workpiece travels past the cutting tool in one minute.
Why does RPM decrease as workpiece diameter increases?
Because a larger diameter workpiece has a larger circumference, each revolution covers more linear feet. To maintain a constant recommended cutting speed (SFM), spindle RPM must decrease proportionally.
How do you convert metric cutting speed (m/min) to RPM?
Use the metric formula: RPM = (V_c × 318.3) / D, where is cutting speed in meters per minute and is diameter in millimeters.
What is G96 on a CNC lathe?
G96 activates Constant Surface Speed (CSS) mode. The CNC lathe control continuously recalculates and adjusts spindle RPM as the cutting tool moves along the X-axis, maintaining consistent surface speed and surface finish.
Ready to run the numbers?
Get your result instantly — private, in your browser.